Choosing the right plastic color masterbatch can determine more than a product’s appearance. It can influence processing stability, recycled-content performance, surface quality, and customer acceptance. A bright blue pellet may look perfect in a sample bag, yet fail after dilution in a thin-wall injection molding process. The problem may involve poor dispersion, an unsuitable carrier resin, or an inaccurate let-down ratio.
Dr. Markus Schmid, a polymer-colour researcher, observes, “A masterbatch succeeds when color, dispersion, and process stability travel together.” This practical view matters when sourcing across borders. Buyers must examine pigment chemistry, carrier compatibility, recommended dosage, heat resistance, lightfastness, and migration requirements. They should also compare L*a*b* color data, technical data sheets, safety documents, certificates of analysis, and production samples. Details matter. Even the packaging can affect results if moisture enters during storage.
Price alone is a weak filter. A cheaper plastic color masterbatch may create purging waste, unstable shades, or rejected batches. That cost appears later. Sometimes, suppliers provide impressive laboratory data but limited evidence from continuous production. This deserves careful questioning. Ask for batch records, reference applications, quality-control methods, and realistic lead times. Confirm whether the supplier can support your target resin, equipment, climate, and annual volume.
There is no universal masterbatch. A solution for polypropylene may perform poorly in polyethylene or engineering plastics. Global sourcing also requires clear communication about specifications, tolerances, documentation, and delivery responsibilities. The best choice balances color accuracy, technical reliability, compliance readiness, and total cost. It may not be the most colorful option. It should be the most dependable one.
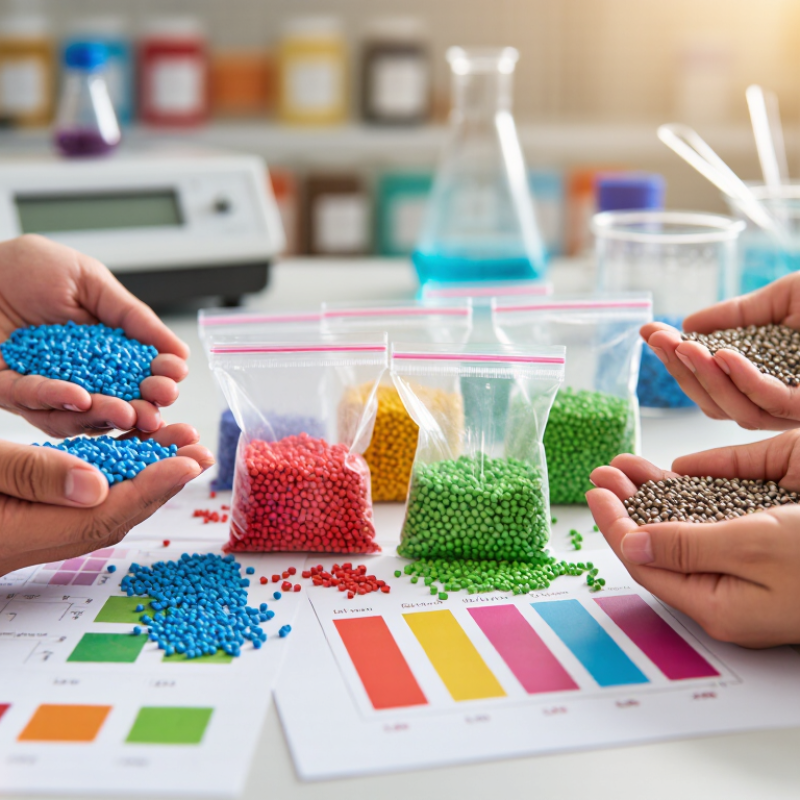
Plastic color masterbatch is a concentrated blend of pigments, additives, and a carrier resin.
It is supplied as small pellets for mixing into base polymers during processing. The carrier must match the target plastic, or dispersion and surface quality may suffer.
Its role in global sourcing goes beyond color. A consistent masterbatch supports repeatable shade, processing efficiency, and easier quality control across factories. Plastics Europe reported global plastics production of 400.3 million tonnes in 2022. That scale makes color consistency a serious supply-chain issue, not a minor design detail.
The OECD’s Global Plastics Outlook also highlights the growing complexity of international plastic flows. Buyers should therefore confirm:
Buyers should confirm these factors before comparing prices. A cheaper product may create higher costs through rejects, purging, or delayed approvals.
Sometimes, the “standard” shade is not standard enough.
Tips:
Request molded plaques from the actual production resin. Compare them under controlled lighting, not beside a warehouse window. Ask for color difference data, such as ΔE values, and define an acceptable tolerance. Check batch traceability and retain an approved reference sample. Independent testing is useful when the application involves heat, outdoor exposure, or sensitive packaging. Do not rely only on a supplier’s color card. It can look perfect on paper.
Choosing a plastic color masterbatch begins with polymer compatibility, not a color chart. The carrier resin should match the base polymer closely. A polyethylene carrier may disperse poorly in nylon or PET. Poor compatibility can cause streaks, weak weld lines, or uneven gloss. Processing temperature matters too. A formulation that survives polypropylene temperatures may degrade during high-temperature engineering plastic production. Small differences matter.
Ask for technical data before comparing prices. Check pigment loading, recommended dosage, moisture content, and thermal stability. For nylon, drying conditions deserve special attention because moisture can change both processing and color. A trial plaque should use the actual resin, machine settings, wall thickness, and surface finish. Test the real material. A laboratory sample can look excellent, yet fail after molding.
End-use requirements should define the color target. Outdoor products need resistance to sunlight, heat, and weathering. Automotive interiors may require low odor, scratch resistance, and stable appearance under repeated heating. Packaging applications often need migration and contact documentation for the intended use. Measure color with a spectrophotometer, not only by eye, and record the light source, gloss, and acceptable ΔE range. One mistake is treating color matching as a visual decision alone. Another is ignoring recycled content, which can shift the final shade between batches. That uncertainty should be discussed openly with the supplier and checked through repeated production trials.
Identify polymer compatibility and end-use color requirements before approving a masterbatch. A higher carrier-match score indicates better polymer compatibility, while a lower ΔE*ab value indicates a tighter color tolerance.
Use the same polymer family and a similar processing-temperature window when selecting the carrier resin. Packaging and automotive applications usually require tighter color control than general consumer products.
When choosing plastic color masterbatch for global sourcing, evaluate pigment quality beyond color samples. Request a recent certificate of analysis, migration data, and heavy-metal test results. Check shade consistency under the intended processing temperature. A sample may look perfect at room temperature but shift during molding. Ask for test plaques made with your actual resin and dosage. Confirm pigment dispersion through microscopy or a controlled production trial. Small agglomerates can create streaks, weak spots, or clogged filters.
Safety documentation should match the product’s final application. Food-contact packaging, children’s products, electrical parts, and outdoor materials require different evidence. Review the safety data sheet, technical data sheet, restricted-substance declarations, and applicable regional requirements. Depending on the destination, this may include REACH, RoHS, food-contact rules, or local chemical inventories. Do not accept a certificate without checking its scope, test date, laboratory, and tested material. Compliance claims can be incomplete. I have seen paperwork that covered the pigment, but not the carrier system.
Tips: Keep a written approval checklist. Record batch numbers, color measurements, dosage, resin type, and processing conditions. Compare retained samples after shipment and production. Ask suppliers how they control raw-material changes. Also question your own assumptions. A lower dosage is not always safer or cheaper if dispersion fails. Build a small trial into the sourcing schedule, even when the sample appears reliable.
Choosing a plastic color masterbatch supplier requires more than comparing prices. I usually examine technical capability before requesting a quotation. Can the supplier match color under different lighting conditions? Can it provide dispersion data, heat resistance results, and batch-to-batch records? A capable team should explain carrier resin compatibility with your production material. It should also send laboratory samples with clear test conditions. Guesswork is expensive.
Cost comparison must include the full sourcing picture. A low kilogram price may hide higher letdown ratios, extra testing, or costly air freight. Ask for pricing at several order volumes, including sample, trial, and regular production quantities. Compare payment terms, packaging, lead time, and replacement procedures for inconsistent batches. Landed cost matters more than the invoice figure. I once focused too heavily on unit price and underestimated the cost of delayed production.
Minimum order quantity can shape your cash flow. Large MOQs may reduce the price but leave slow-moving colors on your shelves. Smaller MOQs offer flexibility, although they can increase production and packaging charges. Request a written MOQ table for standard colors, custom colors, and repeat orders. Also confirm whether the supplier retains color standards for future matching. Details matter here.
Do not rely only on polished sales presentations. Request recent test reports, production photos, and references from comparable applications. A factory visit or independent inspection can reveal practical weaknesses. Some suppliers communicate well but lack stable quality control. I have missed that difference before. Build a comparison sheet, but leave room for uncertainty. Supplier capability, total cost, and MOQ terms should be judged together.
| Anonymous Supplier Profile | Typical Production Focus | Compatible Polymers | Color Matching & Technical Capability | Common Certifications & Compliance Support | Indicative Price Range (USD/kg) |
Typical MOQ | Sample & Color Approval Terms | Standard Lead Time | Payment & Commercial Terms | Best Fit for Global Buyers |
|---|---|---|---|---|---|---|---|---|---|---|
| Large Integrated Producer | High-volume production of standard and custom concentrates with automated dosing, twin-screw extrusion, laboratory testing, and batch traceability. | PE, PP, PS, ABS, SAN, PET, PA, PC, PBT, and selected engineering polymers. | Instrumental color measurement using CIE L*a*b* and ΔE; production control commonly uses spectrophotometers and retained samples. | ISO 9001 REACH support RoHS support SDS/technical files | 1.80–6.50 | 500–1,000 kg per color or formulation; lower quantities may be accepted for repeat programs. | Physical color chips or molded plaques typically supplied; laboratory sample often available at no charge, while courier and custom development fees may apply. | 3–6 weeks for standard colors; 5–8 weeks for new custom formulations. | Usually 30% deposit and 70% before shipment for new accounts; documentary or open-account terms may be negotiated after credit review. | Global programs requiring stable quality, multi-country supply, and long-term color consistency. |
| Regional Custom Compounder | Flexible small-to-medium batch production, custom color development, and application-specific formulations. | PE, PP, ABS, HIPS, PET, PA, PC, POM, and selected biodegradable or recycled resin systems. | Good support for custom matching, opacity adjustment, filler interaction, dispersion optimization, and processing-trial feedback. | ISO 9001 REACH support RoHS support Food-contact review | 2.20–8.00 | 100–500 kg per color; development batches may be available from 25–50 kg. | Usually one to three laboratory iterations; a signed color standard, target resin, let-down ratio, and processing conditions are normally required. | 2–5 weeks for standard formulations; 4–7 weeks for custom colors. | Commonly 30% deposit with balance before dispatch; repeat customers may qualify for 30-day terms subject to approval. | Buyers that need technical collaboration, moderate volumes, and faster custom color development. |
| Export-Oriented Standard Color Supplier | High-output production of catalog colors and commonly requested polymer-specific concentrates. | Primarily PE, PP, ABS, PS, and PVC; narrower coverage for engineering polymers. | Reliable for standard shades and routine applications; custom matching is usually available but may involve fewer trial iterations. | ISO 9001 SDS REACH declarations RoHS declarations | 1.50–4.50 | 300–1,000 kg per color; catalog colors may have lower MOQs when already in production. | Standard color cards or pellets are commonly available; custom samples may require a development charge refundable against a production order. | 2–4 weeks for stock or standard colors; 4–6 weeks for new colors. | Often 30% deposit and 70% before shipment; quotations may be based on FOB, FCA, or CIF terms. | Cost-sensitive importers with repeatable colors and established incoming quality-control procedures. |
| Specialty Engineering-Plastics Formulator | Low-volume, high-performance formulations for demanding temperature, chemical, flame-retardant, or appearance requirements. | PA, PC, PBT, PET, POM, PPS, PEI, PSU, and other engineering thermoplastics. | Supports high-temperature pigments, migration control, warpage considerations, fiber-filled grades, and processing-window optimization. | ISO 9001 UL documentation support REACH support RoHS support | 5.00–18.00 | 100–500 kg per formulation; some specialty colors may require a larger campaign quantity. | Technical sample approval often includes heat-aging, migration, weathering, or processing validation when relevant to the end use. | 4–8 weeks for standard specialty grades; 6–12 weeks for new formulations or qualification work. | Typically deposit-based for development orders; tooling, testing, and qualification charges may be quoted separately. | Automotive, electrical, appliance, medical-device, and other applications with strict performance requirements. |
| Sustainable & Recycled-Resin Specialist | Color concentrates designed for PCR, PIR, bio-based, recycled-content, and mechanically variable resin streams. | Recycled PE, recycled PP, PET, PLA, selected polyamides, and other sustainability-focused resin systems. | Focuses on shade correction, batch-to-batch variation management, odor or contamination considerations, and compatibility with recycled feedstocks. | ISO 9001 Recycled-content support REACH support RoHS support | 2.50–9.00 | 250–750 kg per color; smaller pilot quantities may be possible for qualification projects. | Approval should be based on the actual recycled resin source and target processing conditions; color drift may require a defined tolerance range. | 3–7 weeks, depending on pigment availability and recycled-resin testing requirements. | Usually deposit plus balance before shipment; sustainability documentation and chain-of-custody evidence may be charged or supplied separately. | Brands and converters targeting recycled-content claims, lower-impact packaging, or circular-material programs. |
| Local or Nearshore Distributor with Toll Manufacturing | Regional stocking, technical sales, and outsourced or partner-manufactured color concentrates. | Common packaging and consumer-product polymers such as PE, PP, PET, PS, ABS, and PVC. | Fast commercial support and local troubleshooting; formulation ownership and laboratory depth depend on the manufacturing partner. | SDS REACH support RoHS declarations Local compliance files | 2.80–8.50 | 25–250 kg for stocked items; 100–500 kg for made-to-order colors. | Fast access to stock samples; custom color matching may be coordinated through the toll manufacturer and take longer than local stock delivery. | 1–3 weeks from local stock; 4–8 weeks for made-to-order material. | Often available on local-currency invoices, shorter payment cycles, and delivered-duty or regional freight terms. | Small and medium buyers prioritizing short replenishment times, lower inventory risk, and local technical support. |
A reliable choice starts with a physical sample, not a digital color chart. Request molded plaques in the target resin, using your planned processing temperature. Compare them under daylight and factory lighting. I once approved a sample that looked perfect on my screen. It appeared slightly yellow in production. That mistake delayed a shipment.
Check color difference, dispersion, moisture, and melt flow behavior. Ask for a retained production sample and a clear test report. During a trial run, inspect the first, middle, and final bags. The shade should remain stable. It should also perform consistently after heat exposure and storage. Small variations can become obvious across thousands of parts.
Packaging deserves equal attention. Moisture-resistant bags, readable batch labels, and sealed inner liners protect the material during long transit. Confirm bag weight, pallet dimensions, and stacking limits before booking freight. Request photos after packing. A crushed pallet creates waste before the container leaves port. Share the safety data sheet and technical data sheet with your receiving team. Also agree on shipment terms, lead times, and backup transport plans. My own checklist once missed the local holiday calendar. It was a simple oversight, but the delivery moved by two weeks. Build practical communication into the order, and question every assumption.
WhatsApp us